

Fishing Net Warp Knitting Machine: Gauge, Width and Laserstop

A fishing net line is specified by two numbers and one habit: the gauge that sets how fine the mesh can be, the working width that sets how much net leaves the machine per course, and the stop behaviour that decides how much scrap you make when a yarn breaks at three in the morning. Our fishing net warp knitting machine is built around all three.
Gauge and width: the two decisions everything else follows
The machine is available in gauges E3, E6, E8, E10, E12 and E18, and in working widths of 181, 205, 268, 283, 335, 413 and 503 inches. Those two lists are the frame of the whole specification — bar tooling, yarn path and creel capacity all get sized after they are fixed.
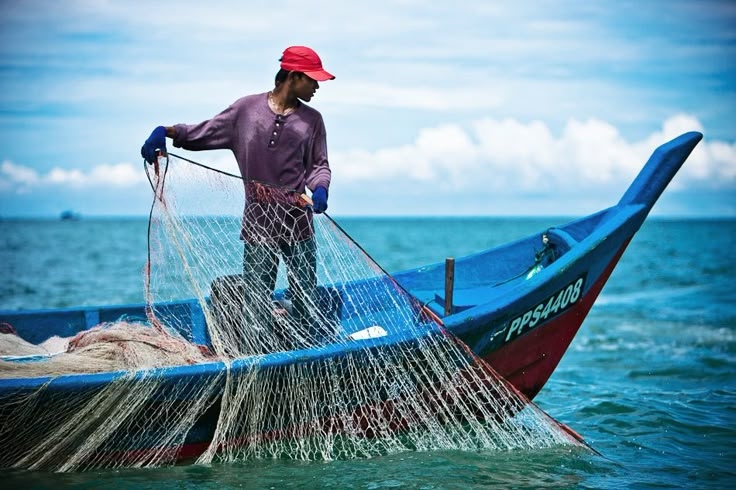
Work from the net, not from the machine. Take the mesh and the yarn you already sell, then the finished panel width your buyers cut from, then add the edge you lose in finishing. That order keeps you from paying for width you trim off every roll, or from ordering a gauge that cannot hold the mesh your customer specified.
| Specification | Options on this machine | What it decides |
|---|---|---|
| Gauge | E3, E6, E8, E10, E12, E18 | How fine a mesh the needle bar can form; the coarse end suits heavy netting, the fine end closer structures. |
| Working width | 181″ to 503″ in seven steps | Panel width per run, creel width, floor length and the size of every doff. |
Latch needles mounted in blocks — or one at a time
The machine knits with latch needles that can be mounted in blocks or inserted individually. That sounds like a detail until the first needle goes down in a wide machine: a block swap gets you running again quickly, while single insertion lets you replace one needle without disturbing the neighbours you have already timed in.
Keep both options in the spares plan rather than picking one. Wide machines lose needles unevenly — usually at the ends of the bar where the yarn path is least forgiving — and the two mounting methods answer two different failure patterns. Related tooling is listed on our latch needle bar page.
Yarn feeding: tension is where net quality is won or lost
The yarn feeding system uses multiple feeding positions and rollers so tension can be held across the width rather than averaged across it. On net structures that matters more than on solid fabric: a slack zone shows up as an uneven mesh only after the panel is stretched, which is to say after it has already been produced.
Set and record the feed positions per article, not per shift. Netting runs long and the operators who set it up rarely doff it, so a written setting sheet per article beats memory every time.
What the Laserstop system actually does
The Laserstop system watches the running machine with sensors and stops it when it detects a fault such as yarn breakage or incorrect tension. It is a stop device first and a safety device second: it halts the machine before a broken end becomes a length of unsellable net, and it takes the operator out of the position of having to notice a fault in time.
The practical payoff is measured in scrap length, so measure it that way. Note the metres of net produced between the fault and the stop before and after, and you will have the only number that settles whether the system is earning its place on your line.
If your situation looks like one of these
If you already run netting and the complaint is inconsistent mesh across the panel, then look at feeding positions and tension across the width before touching gauge — a gauge change is an order, a tension map is an afternoon.
If you are entering netting from another warp knitting product, then decide the mesh and yarn first and let those pick the gauge from the six on offer, because that decision cannot be reversed with settings.
If your bottleneck is downtime rather than mesh quality, then the stop system and the needle mounting method matter more to you than the extra width, and the wider machine will make every stoppage more expensive.
None of this applies to knotted netting: those are a different machine class, and gauge and needle discussions here do not transfer to them.
Support once the machine is on your floor
Service teams are present in more than 20 countries, including Turkey, India, Vietnam, Indonesia and the USA, covering installation, operator training, scheduled maintenance and remote troubleshooting. For a wide netting machine, get the training booked around your own article change-over, not around the installation date — the change-over is where the setting sheets are written.
Neighbouring machine classes are covered on our raschel knitting net machine page and in our net-making machines overview; commercial enquiries and spare-part listings sit on our company site at grandstarcn.com.
Before you ask for a quotation
Send the mesh opening and yarn you produce today, the finished panel width your buyer cuts from, the trim you lose, the shift pattern the line will run, and the space you can give the creel and the doff. With those five, a gauge and a width can be named without a second round of questions.
Frequently Asked Questions
What gauge do I need for my fishing net?
Gauge follows the mesh and the yarn you already sell, not the other way round. This machine is offered in E3, E6, E8, E10, E12 and E18: the coarse end suits heavy netting, the fine end closer structures. Send a sample of the net you produce today and the gauge choice becomes a short conversation.
How wide can the machine go?
Working widths run 181, 205, 268, 283, 335, 413 and 503 inches. Choose from the finished panel width your customer cuts from plus the edge you lose in finishing, and remember that every extra inch of width also lands in the creel, the floor length and the weight of each doff.
What happens when a yarn breaks during the run?
The Laserstop system detects faults such as yarn breakage or incorrect tension and stops the machine automatically, so a broken end does not run on into a length of unsellable net. Track the metres produced between fault and stop if you want a number for what it saves you.
Can I change one needle, or do I have to swap a whole block?
Both. The latch needles can be mounted in blocks or inserted separately, so you can swap a block to get running again quickly, or replace a single needle without disturbing the ones already timed in. Keep spares for both methods.
Do you support the machine after installation?
Service teams are present in more than 20 countries, including Turkey, India, Vietnam, Indonesia and the USA, covering installation, operator training, maintenance and remote troubleshooting. Booking training around your first article change-over gets more out of it than booking it around the installation date.
Hey, I’m Vincent!
Solving complex challenges with precision and creativity in the warp knitting industry. Passionate about advancing textile engineering and turning innovative ideas into reality. Shaping the future of warp knitting.


